Textile dyeing is the process of giving a fibre, yarn, fabric or finished garment an even, lasting colour by letting it take up a dye from a liquid, usually water, and then fixing that dye in the fibre with heat or chemicals and washing off what did not fix. The dye has to suit the fibre: reactive, direct, vat and sulphur dyes colour cotton and other cellulosic fibres, acid dyes colour wool, silk and nylon, disperse dyes colour polyester, and basic dyes colour acrylic. The dye can go on at any stage, as loose fibre, yarn, fabric (piece dyeing) or a sewn garment, either in batches, where the goods sit in a machine with the dye bath for minutes to hours (exhaust dyeing), or continuously, where fabric runs through a pad of dye liquor and on into fixation and washing. This page explains each method, dye class and machine, then works through the calculations a dyer uses every day: liquor ratio, shade percentage, the recipe, fixation, pick-up and colour difference.
Last verified: 14 November 2026. Dye classes, fixation rates and process descriptions come from the US Environmental Protection Agency’s textile industry profile; water use per route from the EU’s best available techniques conclusions for textiles (2022); dye chemistry from peer-reviewed papers and patents. Every source is linked where it is used and listed at the end.

Textile dyeing at a glance
| Question | Short answer | Section |
|---|---|---|
| What is dyeing? | Colouring a textile with a dye the fibre takes up from solution, then fixing and washing it | What is textile dyeing |
| Which dye for which fibre? | Cotton: reactive, direct, vat, sulphur. Wool and nylon: acid. Polyester: disperse. Acrylic: basic | Types of dyes |
| What is exhaust dyeing? | Batch dyeing: the goods sit in the dye bath until the dye has moved from the liquor into the fibre | Exhaust and continuous |
| What are the methods of dyeing? | By stage: stock (fibre), yarn (package, hank, warp), piece (fabric) and garment dyeing; or colour added to the polymer before spinning | Methods by stage |
| Which machines dye fabric? | Jet, winch (beck), jigger and beam machines in batches; pad ranges continuously; rotary drums for garments | Dyeing machines |
| How much dye, salt and water? | Dye = batch weight × shade %. Bath = batch weight × liquor ratio. Worked through below | Dyeing calculations |
| How is the colour checked? | Against the standard by spectrophotometer (Delta E CMC), and for fastness to washing, light and rubbing on ISO 105 grey scales | Shade and fastness |
What is textile dyeing?
Dyeing means colouring a textile all through with a substance that has an affinity for the fibre. In the words of the US Environmental Protection Agency’s description of the industry, the textile is brought to equilibrium, or near it, with a solution of the dye, and “because the dyes have an affinity for the fibers, the dye molecules leave the dye solution and enter the fibers over a period of minutes to hours”; the dye is then fixed with heat or chemicals, and the goods are washed to remove unfixed dye and chemicals (US EPA, Profile of the Textile Industry, 1997, p. 31).
Dye or pigment? The two are often confused, and an older version of this site’s dyeing pages called dye “a pigment”. They are different. A dye dissolves (or is dispersed) in the bath and enters the fibre. A pigment is insoluble, has no affinity for the fibre, and is held on the surface by a resin binder, which is why pigments are used mostly for printing rather than dyeing (US EPA 1997, p. 36). Dyeing colours the whole textile; textile printing puts colour on in a pattern.
Why a dyed fibre looks coloured. Light falling on a fabric is partly reflected, partly absorbed and partly transmitted. A dye absorbs some wavelengths of visible light, and the eye sees the rest that comes back. That is also why colour can be measured with an instrument rather than judged by eye; the site’s guide to colour measurement covers the theory.
A short history. Before the 1850s, dyes came from plants, insects and minerals. The first commercial synthetic dye was mauve, made in 1856 by the 18-year-old William Henry Perkin “from chemicals derived from coal tar” (Science History Institute). Today the industry’s dyes are “largely synthetic, typically derived from coal tar and petroleum-based intermediates”, and are sold as powders, granules, pastes and liquid dispersions with 20 to 80 percent active ingredient (US EPA 1997, p. 31). Natural dyes are covered in the site’s guide to natural dyes and plant colorants.
Types of dyes and the fibres they dye
Dyes are grouped by the fibres they can colour and the way they are applied. The first four columns of the table are the EPA’s own table of dyes used in textile dyeing (US EPA 1997, table 6, p. 35, compiled from EPA’s 1995 pollution prevention guide and Snowden-Swan 1995). Fixation is the share of the dye put into the bath that ends up fixed on the fibre; the rest leaves in the waste water. The last column says how the dye holds, from the sources named in it.
| Dye class | Fibres it dyes | Usual method | Typical fixation | How it holds in the fibre |
|---|---|---|---|---|
| Reactive | Cotton, other cellulosics, wool | Exhaust, cold pad-batch, continuous | 60–90% | Forms a covalent bond with the hydroxyl groups of cellulose. Salt is added to drive the dye onto the fibre, alkali (soda ash or caustic soda) to fix it (Moula et al. 2022; Negi 2025) |
| Direct | Cotton, rayon, other cellulosics | Exhaust, continuous | 70–95% | Water-soluble and anionic; applied straight to cellulose without a mordant. The simplest and cheapest to apply, at some cost in shade range and wet fastness (EPA 1997, p. 34) |
| Vat (indigo is one) | Cotton, other cellulosics | Exhaust, package, continuous | 80–95% | Insoluble in water. Reduced in an alkaline bath to a soluble “leuco” form, taken up, then oxidised back to the insoluble colour in the fibre by air (US 5,611,822) |
| Sulphur | Cotton, other cellulosics | Continuous | 60–70% | Applied, like vat dyes, with a reducing agent such as sodium sulphide or hydrosulphite (Decision (EU) 2022/2508, BAT 41) |
| Acid | Wool, nylon (and silk) | Exhaust; continuous for carpet | 80–93% | Applied in an acid bath, where the amino groups of the fibre are protonated and hold the anionic dye by ionic bonds (Negi 2025) |
| Basic (cationic) | Acrylic, some polyesters | Exhaust | 97–98% | Water-soluble, applied in weakly acidic dyebaths; very bright colours (EPA 1997, p. 35) |
| Disperse | Polyester, acetate, other synthetics | High-temperature exhaust, continuous | 80–92% | Not water-soluble and non-ionic. Polyester takes it up above its glass transition, so it is dyed at about 130 °C under pressure (Rahman et al. 2025), or with “carriers” at lower temperature, which the EU best available techniques avoid for polyester without wool (BAT 43) |
Two notes on the table. The EPA text on the page before it gives direct dyes 90–95% fixation while its own table gives 70–95%; this page uses the table. And reactive dyes, the EPA’s “largest dye class”, lose the most dye: at 60% fixation, two-fifths of the dye put into the bath never fixes and leaves in the spent bath and the wash-off water, which is the effluent problem worked through in the fixation example below. Mordant dyes, the old way of fixing many natural dyes, work by forming complexes with metal salts (Negi 2025). For the chemistry behind each class see fundamentals of dye chemistry and types of dyes by chemical structure; for why the same dye goes on differently to cotton, wool and polyester, see fibre morphology and dye uptake.
Dyeing wool. Wool is dyed with acid dyes and reactive dyes (US EPA 1997, table 6), and with metal-complex and chrome mordant dyes. The EU’s best available techniques for wool put reactive dyeing without a chromium mordant first, then optimised metal-complex dyeing, and allow dichromate mordants only where they are authorised and dosed to the dye actually taken up (Decision (EU) 2022/2508, BAT 42). The fibre itself is described in the site’s guide to wool.
Exhaust dyeing and continuous dyeing: the principles
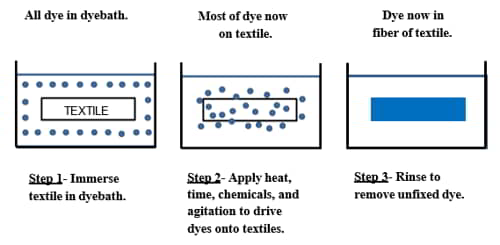
Exhaust (batch) dyeing. A batch of textile, usually 100 to 1,000 kilograms, is loaded into a machine with water, dye and auxiliary chemicals. Heat, time, chemicals and the movement of goods or liquor drive the dye out of the bath and into the fibre; the bath is then dropped and the goods rinsed (US EPA 1997, p. 31). “Exhaust” names what happens to the bath: a well-run dyeing leaves little dye in it. The common batch methods are beam, beck (winch), jet and jig dyeing.
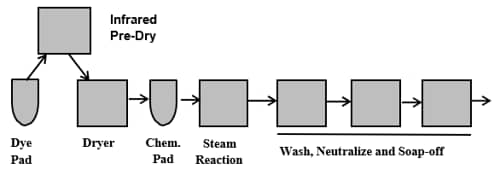
Continuous dyeing. Fabric runs through a dye range at, usually, 50 to 250 metres a minute: the dye is applied in a pad (a trough and a pair of squeeze rollers), fixed by heat or chemicals, often in steam, and washed. In the EPA’s 1997 account continuous dyeing made about 60 percent of the yardage dyed in the US industry, but a dyer needed runs of 10,000 metres or more per colour to make it pay, with specialty ranges then being designed for 2,000 metres (US EPA 1997, p. 31, citing Snowden-Swan 1995). Short runs and many colours therefore go to batch machines.
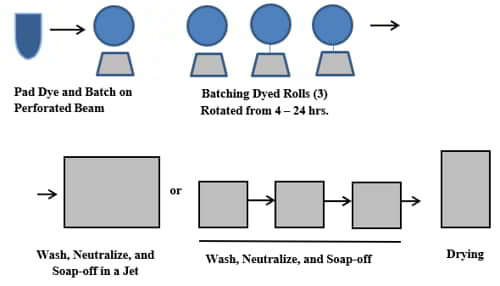
Pad-batch dyeing sits between the two. Fabric is padded with dye and alkali, wound on a roll and slowly turned at room temperature for hours, then washed. The EU names this cold pad-batch technique a best available technique because it needs fewer chemicals and no thermal fixation (Decision (EU) 2022/2508, section 1.9.4).
Methods of dyeing by stage: fibre, yarn, fabric and garment
Colour can go into a textile at any stage of its making. The later the stage, the later the colour decision can be made; the earlier, the deeper and more even the colour usually is, and the more patterns become possible from coloured yarns.
| Stage | What is dyed | Why it is used |
|---|---|---|
| Dope dyeing (mass coloration) | Man-made fibre: colorant mixed into the polymer melt before the fibre is spun | No dye bath; the colour is part of the fibre (Balakrishnan et al. 2022) |
| Stock dyeing; top dyeing | Loose fibre; combed wool sliver (tops) (EPA 1997, p. 31) | Colour right through the fibre, and differently coloured fibres can be blended into one yarn |
| Yarn dyeing | Yarn on packages, in hanks (skeins) or on warp beams | Checks, stripes and plaids woven or knitted from coloured yarns; sewing thread and knitting yarn |
| Piece dyeing (fabric dyeing) | Woven or knitted fabric | Most dyed fabric, because it gives “maximum inventory flexibility to meet color demands as fashion changes” (EPA 1997, p. 32) |
| Garment dyeing | Sewn garments | The latest possible colour decision, and garments sold together match exactly |
Yarn dyeing: package, hank (skein) and warp dyeing
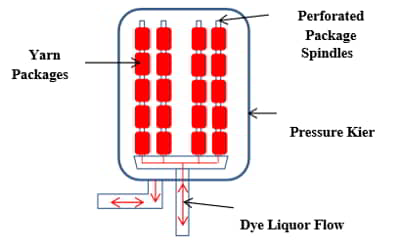
In package dyeing spools of yarn are stacked on perforated rods and the dye is forced outward through them under pressure, then back toward the centre, so that it penetrates the whole package; “most carded and combed cotton used for knitted outerwear is package-dyed”. In skein (hank) dyeing the yarn is loosely coiled into skeins hung over a rung in the dyebath, the method used for bulky acrylic and wool yarns (US EPA 1997, p. 32). The site’s article on the factors that affect yarn dyeing goes further.
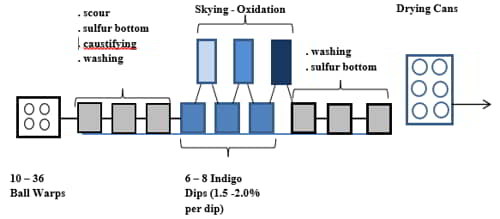
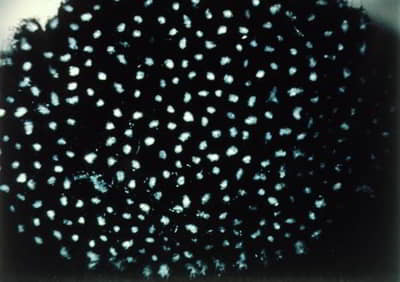
Indigo warp dyeing for denim is a continuous yarn process. Warp yarns are dipped in a vat of reduced indigo, squeezed between rolls and carried into the air, where the leuco dye oxidises back to blue indigo in the fibre, a step called “skying”; the dip-and-sky cycle is repeated to build the shade (US 5,611,822). Indigo “tends to dye the outside of the fiber bundle” of a ring-spun cotton yarn, leaving a pale core; wearing or abrading the surface exposes that core, which is how denim fades, and one patent puts the undyed core of standard commercial indigo dyeing at 45 to 60 percent (US 5,514,187, Burlington Industries). More in the site’s guide to indigo dyeing for denim, and the indigo rope oxidation calculator.
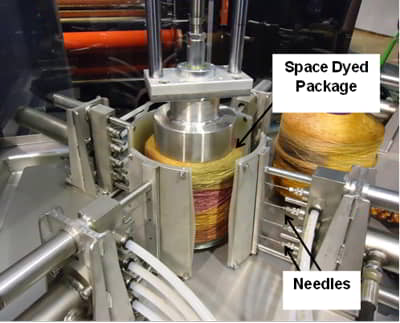
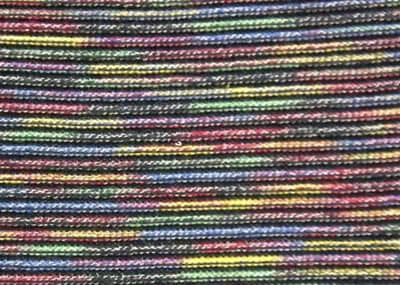
Space dyeing is “the production of yarn having different dyes spaced along its length”; in batch versions, yarn packages are injected with several dyes of different colours (US 6,413,632, Milliken). Knitted up, the yarn gives the random multicoloured streaks below.
Piece dyeing (fabric dyeing) and cross-dyeing
Piece dyeing means dyeing fabric after it has been woven or knitted. Most dyed fabric is piece-dyed, because a mill can hold undyed fabric and dye it to whichever colours sell (US EPA 1997, p. 32). It runs in batches on the jet, winch, jigger and beam machines below, or continuously on a pad range. A fabric woven from two fibres that take dye differently can be cross-dyed in one bath, so that a single dyeing gives a check or stripe; dyeing both fibres to one shade (union dyeing) is the opposite aim, and the blends section shows how polyester/cotton is done.
Garment dyeing
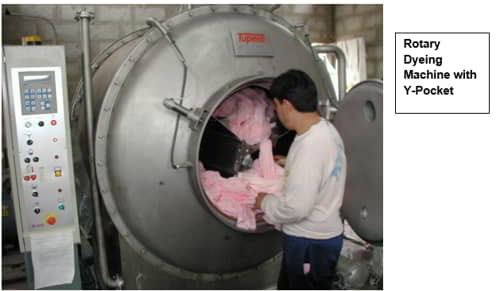
Garments sewn from prepared, undyed fabric are dyed whole in a rotary drum or paddle machine. The colour decision is made at the last moment, and pieces sold together match because they were dyed together. Seams, threads and trims must take the dye, or be chosen not to. Garment washing, which often follows, is in the site’s article on dyeing and washing in garment manufacturing.
Dyeing machines
A dyeing machine has one job: bring every part of the goods into contact with the same liquor for the same time at the same temperature. It does that either by moving the goods through still liquor or by pumping liquor through still goods.
| Machine | Goods | What moves | Notes |
|---|---|---|---|
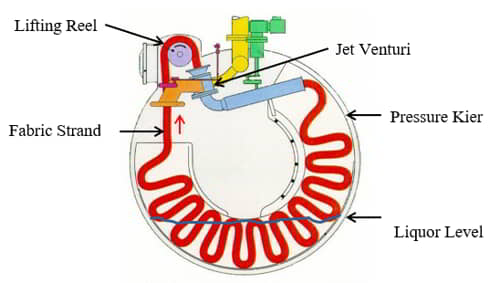
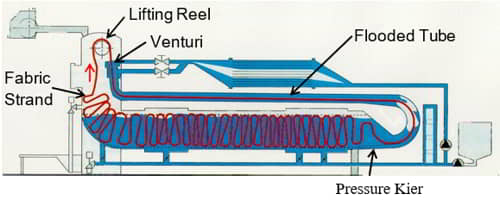
| Jet (and overflow, soft-flow, air-flow) | Fabric in rope form | Both: liquor jetted through a venturi carries the fabric rope round a closed kier | Pressurised versions dye polyester at about 130 °C |
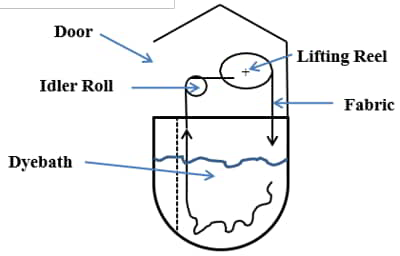
| Winch (beck) | Fabric in rope form | Fabric: a reel lifts the rope out of the bath and drops it back in | The fabric is lifted and dropped rather than driven by a jet |
| Jigger (jig) | Woven fabric at full width | Fabric: wound from one roller to the other through a shallow bath, back and forth | Open width avoids rope creases (EPA 1997, p. 32) |
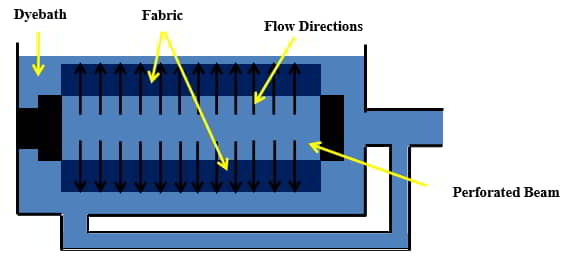
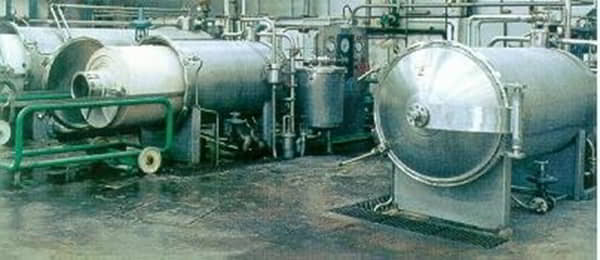
| Beam | Fabric wound on a perforated beam | Liquor: pumped through the roll | The fabric stays still and flat on the beam |
| Package; hank | Yarn | Liquor through packages; or hanks hung in the bath | See yarn dyeing |
| Pad (padder or foulard) | Fabric at full width | Fabric through a trough and squeeze rollers | Continuous and pad-batch dyeing. The squeeze sets the wet pick-up |
| Rotary drum, paddle | Garments | The drum or paddle tumbles the garments | Garment dyeing and washing |

The dyeing process step by step
- Preparation. Fabric must be clean and absorbent before it will dye evenly. The steps, as the EPA describes them: singeing burns protruding fibres off woven goods over a flame or hot plates; desizing removes the size put on warp yarns for weaving (starch sizes on cotton are broken down by enzymes into water-soluble sugars and washed out); scouring uses alkali, typically sodium hydroxide, to remove oils, waxes and dirt; bleaching removes natural colour, and hydrogen peroxide accounted for over 90 percent of the bleach used on cotton and its blends; mercerising treats cotton in cold 15 to 20 percent caustic soda under tension, so that the flat, twisted fibre swells round, gains lustre, strength (by as much as 20 percent) and affinity for dyes (US EPA 1997, pp. 29–30). Desizing and scouring are often combined. The scouring and bleaching recipe calculator and the mercerisation calculator cover the numbers.
- Recipe and lab dip. The shade is matched in the laboratory first, on a small sample, and the recipe scaled to the batch (calculations).
- Dyeing. Dye and auxiliaries go into the bath, and time, temperature, pH and liquor movement are controlled to a programme so that the dye goes on evenly rather than rushing onto the first fibre it meets.
- Fixation. Alkali for reactive dyes, oxidation for vat and sulphur dyes, heat for disperse dyes on polyester.
- Wash-off. Unfixed dye is rinsed and soaped off; left in, it bleeds in the first wash. EU best practice rinses reactive dyeings hot, up to about 95 °C, without detergent, and recovers the heat (Decision (EU) 2022/2508, BAT 41).
- Drying and finishing. The dyed fabric is dried and finished; see textile finishing processes and the overview of fabric wet processing.
Dyeing calculations: liquor ratio, shade percentage and the recipe
Three numbers define a batch dyeing. The liquor ratio is the weight of dry textile to the weight of liquor, written 1:8 for 8 litres of bath per kilogram of goods (the EU defines it as the “weight ratio between the dry textile materials and the process liquor used”, Decision (EU) 2022/2508, definitions). The shade percentage, or depth of shade, is the weight of dye as a percentage of the weight of fibre (% owf, on weight of fibre). Auxiliaries such as salt and alkali are dosed in grams per litre of bath. Each example below was opened in the site’s calculator with the inputs in its link, and the calculator showed the figures quoted.
Worked example 1: a reactive dyeing recipe
A 200 kg batch of cotton knit is dyed at a liquor ratio of 1:8 to a 3% shade with a reactive dye of standard (100%) strength, using 60 g/L of salt and 20 g/L of soda ash. The salt and alkali figures are the calculator’s defaults, used here only to show the arithmetic; the dye maker’s recipe card sets them for each dye and depth.
- Bath volume = 200 kg × 8 = 1,600 L
- Dye = 200 kg × 3 / 100 = 6.00 kg (at 150% commercial strength it would be 6.00 × 100 / 150 = 4.00 kg)
- Salt = 1,600 L × 60 g/L = 96 kg; soda ash = 1,600 L × 20 g/L = 32 kg
- Dye concentration in the bath = 6,000 g / 1,600 L = 3.75 g/L
Check it in the dyeing recipe calculator, prefilled with this batch. At the Zhengzhou soda ash settlement of 974 CNY per tonne on 6 November 2026 (soda ash price), the 32 kg of alkali cost about 31 CNY. Note that the salt and alkali scale with the bath, not the fabric: the same shade at 1:5 needs 1,000 L, so 60 kg of salt and 20 kg of soda ash. The salt, alkali and pH buffer calculator takes the chemistry further.
Worked example 2: liquor ratio and water
The same 200 kg batch at 1:8, followed by five rinse fills of the same volume: 1,600 L × (1 + 5) = 9,600 L, or 48 litres of water per kilogram of fabric (liquor ratio calculator, 1:8). On a low-liquor-ratio machine at 1:5 the same programme uses 1,000 L × 6 = 6,000 L, or 30 L/kg (the same at 1:5), and the salt, alkali and steam to heat the bath fall in proportion. For scale, the EU’s indicative levels for batch dyeing of fabric run from 10 to 150 cubic metres per tonne, which is litres per kilogram (water section).
Worked example 3: exhaustion and fixation
Exhaustion is the share of dye that left the bath; fixation is the share still on the fibre after soaping. Suppose a reactive dyeing starts with 100 units of dye, 20 units are left in the spent bath and soaping removes another 10. Then exhaustion = (100 − 20) / 100 = 80%, fixation on the dye applied = (100 − 20 − 10) / 100 = 70%, fixation on the dye exhausted = 70 / 80 = 87.5%, and 30% of the dye bought goes to the effluent (exhaustion and fixation calculator). A 70% fixation is inside the EPA’s 60–90% range for reactive dyes. The reactive wash-off calculator shows how much water it takes to rinse the unfixed 30% out.
Worked example 4: wet pick-up on a pad
In pad dyeing the shade is set by how much liquor the fabric carries out of the nip, not by a liquor ratio. A 100 g sample that weighs 165 g after padding has a wet pick-up of (165 − 100) / 100 = 65%, so each kilogram of fabric carries 0.65 L of liquor. Padding 1,000 kg with a liquor holding 30 g/L of dye takes 650 L of liquor and puts 650 × 30 / 1,000 = 19.5 kg of dye on the fabric, a 1.95% shade (pad-batch pick-up calculator). An uneven nip across the width gives a side-to-centre shade difference that batching cannot correct.
More formulas, from heat-setting to finishing add-on, are collected in dyeing and finishing calculations.
Dyeing polyester/cotton and other blends
Each fibre in a blend needs its own dye class, so a polyester/cotton fabric is dyed twice over: disperse dye for the polyester, reactive (or vat, sulphur or direct) dye for the cotton. A DyStar patent sets out the three standard exhaust routes (US 5,693,103):
- Two-bath: the polyester is dyed first with disperse dye at pH 5–7 and 120–140 °C; the bath is replaced and the cotton is dyed with reactive dye under alkaline conditions.
- Reverse two-bath: the cotton first with reactive dye, then the polyester with disperse dye in a fresh bath.
- One-bath, two steps: the cotton is dyed under alkaline conditions, the same bath is acidified, and the disperse dye is added to dye the polyester at 120–130 °C.
The one-bath routes save time, water and energy, but only work with dyes that tolerate both sets of conditions. The fibres are described in the site’s guides to polyester and cotton.
Shade matching and colour fastness
Shade matching. A dyed batch is measured with a spectrophotometer and compared with the approved standard as CIELAB co-ordinates: L* (light to dark), a* (green to red) and b* (blue to yellow). The plain distance between the two, Delta E*ab, treats every direction alike, but the eye does not, so textile colour difference is judged with the CMC(l:c) formula, which weights lightness, chroma and hue separately; ISO 105-J03 is the standard for the calculation (ISO 105-J03). The lab dip adjustment tool helps correct a recipe that is off-shade.
Worked example 5: is the navy batch on shade?
A navy standard measures L* 30, a* 2, b* −25; the batch measures L* 30.8, a* 1.5, b* −24.0. The batch is 0.80 lighter and 1.03 less saturated, with a hue difference of 0.43. Delta E*ab is 1.37, but with the calculator’s default weights (l = 2, c = 1) Delta E CMC is 0.85, inside a tolerance of 1.0 by 0.15 (Delta E CMC calculator). The tolerance itself is the buyer’s to set; 1.0 is only the calculator’s default.
Colour fastness is how well the colour survives use. The ISO 105 series holds the tests; common ones are washing (ISO 105-C06), light (ISO 105-B02, xenon arc, judged against blue wool references), rubbing or crocking (ISO 105-X12) and perspiration (ISO 105-E04). Change in colour is rated on a grey scale whose essential form has 5 steps of paired grey chips, with four half-steps added in a 9-step version (ISO 105-A02; ISO 105-A02:1993 abstract); staining of the adjacent white cloth is rated on a second grey scale (ISO 105-A03). Grade 5 is a pair of identical chips, meaning no change (AATCC, gray scale). The site’s blue wool lightfastness and crocking fastness calculators help read results.
Hand dyeing techniques: tie-dye, batik, shibori and dip dyeing
Hand and craft dyeing make patterns by stopping the dye reaching parts of the cloth, which is why they are called resist dyeing.
- Tie-dye and shibori. The cloth is tied, folded, bound or stitched before dyeing so that the dye cannot reach the protected parts. In nui shibori, “a stitch-resist form of the ancient Japanese shibori tie-dying technique”, sections of cloth “are gathered together with a running stitch before being dyed” (Cooper Hewitt, Smithsonian Design Museum). Tritik is the same idea, with tightly pulled stitches as the resist. Untie, re-tie and dye again for a second colour.
- Batik. Designs are drawn on the cloth with “dots and lines of hot wax”, which “resists vegetable and other dyes”; the cloth is soaked in one colour, the wax removed with boiling water, and the process repeated for more colours. UNESCO inscribed Indonesian batik on its list of the intangible cultural heritage of humanity in 2009 (UNESCO). See how to make batik designs.
- Dip dyeing. Only part of the cloth is lowered into the bath, or parts are dipped for longer, so the colour grades from deep to pale; a second colour can be dipped from the other end.
- Natural dyes. Many natural dyes are applied with a mordant, a metal salt that forms a complex with the dye (Negi 2025). See the guides to natural dyes and natural indigo.

Water, effluent and lower-impact dyeing
Wet processing is measured in water used per tonne of textile. The EU’s best available techniques conclusions for the textiles industry give indicative yearly averages for water use per tonne of textile processed (Commission Implementing Decision (EU) 2022/2508, table 1.1). A cubic metre per tonne is a litre per kilogram:
| Process | Indicative water use (m³ per tonne) |
|---|---|
| Batch dyeing, fabric | 10–150 |
| Batch dyeing, yarn | 3–140 |
| Batch dyeing, loose fibre | 13–60 |
| Continuous dyeing | 2–16 (up to 100 for plants combining continuous and batch processes) |
| Bleaching, batch; continuous | 10–32; 3–8 |
| Scouring of cellulosic materials, batch; continuous | 5–15; 5–12 |
| Combined bleaching, scouring and desizing of cellulosics | 9–20 |
| Mercerisation | 2–13 |
The lower ends assume a high level of water recycling. The levers the same document names are low-liquor-ratio machines, low-volume application on continuous ranges, cold pad-batch dyeing, reuse of process liquor, poly-functional reactive dyes with higher fixation, and polyester dyeing at high temperature without carriers (Decision (EU) 2022/2508, BAT 10 and BAT 40–43). The effluent carries the unfixed dye, salt and alkali; the ZDHC wastewater guidelines set wastewater limits that brands can ask their dyehouses to meet. The site’s water footprint per kilogram of dyed fabric calculator puts a figure on a mill’s own process.
Dyeing with little or no water, using supercritical carbon dioxide, foam or air instead, is a separate subject with its own page: waterless dyeing technologies, with the supercritical CO₂ dyeing calculator. Broader changes are in sustainable textile dyeing and sustainable and eco-friendly textiles.
Questions people ask about textile dyeing
What is the meaning of dyeing in textiles?
Dyeing is colouring a fibre, yarn, fabric or garment with a dye that the fibre takes up from a solution and holds, so that the colour runs through the material rather than sitting on its surface. The dye is then fixed and the excess washed off. Printing, by contrast, applies colour only where the pattern needs it.
What is exhaust dyeing?
Exhaust dyeing is batch dyeing: the goods are held in a machine with the dye bath, and heat, time, chemicals and agitation move the dye from the liquor into the fibre until the bath is nearly exhausted. The dye is then fixed and the goods rinsed. Jet, winch, jigger, beam and package machines all dye by exhaustion.
What is piece dyeing?
Piece dyeing is dyeing fabric after it has been woven or knitted, in batches or continuously. Most dyed fabric is made this way because the mill can keep fabric undyed and colour it when orders come in.
What is skein dyeing, and what is stock dyeing?
Skein (hank) dyeing dyes yarn loosely coiled in skeins hung in the dyebath, and is used for bulky acrylic and wool yarns. Stock dyeing dyes loose fibre before it is spun, so that differently coloured fibres can be blended into one yarn.
What are the main types of dyeing methods?
By process, exhaust (batch), continuous and pad-batch dyeing. By stage, dope dyeing of the polymer, stock dyeing of fibre, yarn dyeing (package, hank, warp), piece dyeing of fabric and garment dyeing. By hand, resist methods such as tie-dye, batik and shibori.
How much dye do I need for a batch?
Multiply the dry weight of the goods by the shade percentage: 200 kg at a 3% shade needs 6 kg of dye at standard strength, less for a stronger commercial brand. Salt and alkali are dosed per litre of bath, so they depend on the liquor ratio. The dyeing recipe calculator does both.
Related on this site
- Fundamentals of dye chemistry: reactive, disperse, acid and types of dyes by chemical structure
- Fibre morphology and its effect on dye uptake and factors affecting the dyeing of yarn
- Basic concepts of colour measurement
- Fabric wet processing techniques, textile finishing processes and the textile manufacturing process
- Waterless dyeing technologies and sustainable textile dyeing
- Textile printing and batik designs
Sources
- US Environmental Protection Agency, Office of Compliance, Profile of the Textile Industry, Sector Notebook Project, EPA/310-R-97-009, September 1997: preparation pp. 29–30, dyeing pp. 31–32, table 6 p. 35, printing p. 36.
- Commission Implementing Decision (EU) 2022/2508 of 9 December 2022 establishing the best available techniques (BAT) conclusions for the textiles industry, OJ L 325, 20.12.2022: definitions, table 1.1, section 1.9.4, BAT 10 and BAT 40–43.
- A. T. M. G. Moula et al., “Effect of dye bath pH in dyeing of cotton knitted fabric with reactive dye (Remazol Yellow RR) in exhaust method“, Heliyon 8 (2022) e11246.
- A. Negi, “Environmental Impact of Textile Materials: Challenges in Fiber–Dye Chemistry and Implication of Microbial Biodegradation“, Polymers 17 (2025) 871.
- Rahman et al., Molecules 30 (2025) 3578, open copy (polyester glass transition and disperse dyeing at about 130 °C).
- N. K. Balakrishnan et al., “Effect of Colorants and Process Parameters on the Properties of Dope-Dyed Polylactic Acid Multifilament Yarns“, Polymers 14 (2022) 5021.
- Patents: US 5,611,822 (indigo dye process, priority 1993); US 5,514,187 (reduced indigo dye penetration, Burlington Industries, filed 1994); US 6,413,632 (space dyed yarn, Milliken, filed 2001); US 5,693,103 (dyeing polyester/cotton blends, DyStar, filed 1997).
- Colour fastness: ISO 105-A02:1993 abstract (New Zealand Building CodeHub); AATCC, gray scale product information; the site’s standards records for ISO 105-A02, A03, B02, C06, E04, J03 and X12.
- History and craft: Science History Institute, William Henry Perkin; UNESCO, Indonesian Batik; Cooper Hewitt, Shibori Stripe.
- Prices: the site’s soda ash and caustic soda series (Zhengzhou Commodity Exchange settlements).
How this page is kept
Last verified: 14 November 2026. Dye classes, fixation ranges and process descriptions are the US EPA’s, from a 1997 profile that is still the most complete public description of textile wet processing; figures from it are given with its date. Water use per process is the EU’s 2022 indicative range. Mechanisms are taken from the peer-reviewed papers and patents linked where they are used. The figures in the diagrams are those of the original drawings. The worked examples use the site’s calculators as they stood on this date, and each prefilled link was opened to check that it shows the figures quoted. The soda ash price is an exchange settlement and moves daily.
Change log. 14 November 2026: rewritten in full, and three overlapping articles on the same subject (Textile Dyeing, Dyeing Methods, and Textile Product Dyeing and Finishing) were merged into this page with their diagrams. Corrected from the earlier versions: dyes and pigments are different things, and dyes are not “pigments”; the direct-dye fixation range follows the EPA’s table (70–95%), not the 90–95% of its text; the machine capacities quoted from a 1975 textbook were dropped as out of date. A claimed 30 percent gain in colour uniformity at an unnamed mill, other unsourced case studies, and a photograph credited to another company’s website were withdrawn.
Found an error, or a newer figure? Please tell us through the contact page, naming the section and the source that disagrees.